Ecer asks for your consent to use your personal data to:
Personalised advertising and content, advertising and content measurement, audience research and services development
Store and/or access information on a device
Your personal data will be processed and information from your device (cookies, unique identifiers, and other device data) may be stored by, accessed by and shared with 135 TCF vendor(s) and 65 ad partner(s), or used specifically by this site or app.
Some vendors may process your personal data on the basis of legitimate interest, which you can object to by do not consent. Contact our platform customer service, you can also withdraw your consent.
Your message must
be between 20-3,000 characters!
Submit Requirement
Thank You!
Your requirement has been sent. we will contact you quickly!
{"title":"Adult Finger Clip SpO2 Sensor Probe 7 Pin For Mindray T5 T8 ECG Monitors","imgUrl":"https:\/\/img.chinax.com\/nimg\/bb\/9f\/950d5a5acf5cdee7705fb5a447ee-200x200-1\/adult_finger_clip_spo2_sensor_probe_7_pin_for_mindray_t5_t8_ecg_monitors.jpg","attrs":{"Compatibility":"Compatible with multiple patient monitors","Operating Temperature":"0\u00b0C to 40\u00b0C","Lead Cable Color":"Gray","Feature":"Disposables"}}
{"title":"Genuine GE B450 650 ECG Monitor Adult Finger Type Pulse Oximeter Sensor TS-SA4-GE","imgUrl":"https:\/\/img.chinax.com\/nimg\/4a\/95\/25f96bd612be0a31e731d158534a-200x200-1\/genuine_ge_b450_650_ecg_monitor_adult_finger_type_pulse_oximeter_sensor_ts_sa4_ge.jpg","attrs":{"Place of Origin":"CHINA","Minimum Order Quantity":"1 PC","Length":"3m \/ 10ft","Connector Distal":"Flat, 11-pin, dual-keyed GE connector"}}
{"title":"Adult Pediatric Defibrillator Pads OBS-DE\/P With Self Test Function For Primedic M250","imgUrl":"https:\/\/img.chinax.com\/nimg\/2e\/24\/28cfab3d974222a0e348f103b40d-200x200-1\/adult_pediatric_defibrillator_pads_obs_de_2fp_with_self_test_function_for_primedic_m250.jpg","attrs":{"Model Number":"M250 Series","Shelflife":"24 months","Place of Origin":"CHINA","Delivery Time":"5-8work days"}}
{"title":"Compatible Surface Temperature Probe Adapter Cable YSI400 For Comen Patient Monitors","imgUrl":"https:\/\/img.chinax.com\/nimg\/c5\/56\/ae6dd7e759578b0d80b5425111df-200x200-1\/compatible_surface_temperature_probe_adapter_cable_ysi400_for_comen_patient_monitors.jpg","attrs":{"Certification":"CE","Minimum Order Quantity":"1 PC","Cable Length":"1.5 meters","Payment Terms":"D\/A,D\/P,T\/T"}}
{"title":"Compatible With PH-ILIPS Mindray 78205 78345 IBP Cables Round 12 Pin To Abbott","imgUrl":"https:\/\/img.chinax.com\/nimg\/c1\/59\/475617261887cf9a6ec9d3317789-200x200-1\/compatible_with_ph_ilips_mindray_78205_78345_ibp_cables_round_12_pin_to_abbott.jpg","attrs":{"Model Number":"12-Pin to Abbott Adapter","Minimum Order Quantity":"1 PC","Place of Origin":"CE","Instrument Classification":"Class I"}}
{"title":"Nihon Kohden Genuine AED-3100 Defibrillator Battery 4 Year Shelf Life SB-310V","imgUrl":"https:\/\/img.chinax.com\/nimg\/77\/1c\/36577d3daa79d584e14d34c2bc9f-200x200-1\/nihon_kohden_genuine_aed_3100_defibrillator_battery_4_year_shelf_life_sb_310v.jpg","attrs":{"Normal Capaicty":"2600mAh","Discharging Current":"0.2A","Certification":"CE","Price":"RMB 3051"}}
{"title":"12 Lead Holter ECG Patient Cable With Gushan Fengbo ITengo+ And BS6930 Holter ECG Recorders","imgUrl":"https:\/\/img.chinax.com\/nimg\/b6\/e2\/b1ccad711a04ce7eddee7caeffa4-200x200-1\/12_lead_holter_ecg_patient_cable_with_gushan_fengbo_itengo_2b_and_bs6930_holter_ecg_recorders.jpg","attrs":{"Delivery Time":"5-8 work days","Price":"RMB 201.14","Memorycapacity":"4GB to 16GB","Displaytype":"LCD or OLED screen"}}
{"title":"GE MAC 500 MAC 1100 Compatible ECG Cable 10 Lead AHA Standard","imgUrl":"https:\/\/img.chinax.com\/nimg\/3d\/9c\/3230a33ae9d9b4cd43aba7938eda-200x200-1\/ge_mac_500_mac_1100_compatible_ecg_cable_10_lead_aha_standard.jpg","attrs":{"Minimum Order Quantity":"1 PC","Sample":"Offered","Cable Type":"Patient Monitoring Cable","Weight":"Lightweight, approximately 50-100 grams"}}
{"title":"Double Tube Small Adult Pediatric NIBP Cuff 2752 17-25cm With Male Female Connectors","imgUrl":"https:\/\/img.chinax.com\/nimg\/f3\/09\/9d2424d7de47722b89a01393a923-200x200-1\/double_tube_small_adult_pediatric_nibp_cuff_2752_17_25cm_with_male_female_connectors.jpg","attrs":{"Storage":"Individually Sealed in PE Bag","Primary Feature":"Primary Feature","Price":"USD 17.6-50","Supply Ability":"1000PCS per month"}}
{"title":"NIBP Blood Pressure Main Extension Tube For Edan IM9A IM8 IM8B M50 IM50 Patient Monitors","imgUrl":"https:\/\/img.chinax.com\/nimg\/3f\/c9\/fdb1295e070756f0d0af19366f4d-200x200-1\/nibp_blood_pressure_main_extension_tube_for_edan_im9a_im8_im8b_m50_im50_patient_monitors.jpg","attrs":{"Model Number":"NIBP Blood Pressure Main Extension Tube","Warranty":"12 month","Temperaturerange":"-20\u00b0C to 60\u00b0C","Length":"120 cm"}}
{"title":"F6\/F6E\/F9\/F9E Maternal Fetal Heart Rate Monitoring Probe Dual Slot 6 Pin US Probe","imgUrl":"https:\/\/img.chinax.com\/nimg\/74\/04\/8fdcfb20a8779a9f058e19e22519-200x200-1\/f6_2ff6e_2ff9_2ff9e_maternal_fetal_heart_rate_monitoring_probe_dual_slot_6_pin_us_probe.jpg","attrs":{"Supply Ability":"1000","Delivery Time":"5-8 work days","Warranty":"1 Year Manufacturer Warranty","Model Number":"Dual-Slot 6-Pin US Probe"}}
{"title":"Original End Tidal CO2 Microstream Adult Sensor M1920A For PH-ILIPS Patient Monitors","imgUrl":"https:\/\/img.chinax.com\/nimg\/a4\/37\/75e5cea416ebb245ac966b446991-200x200-1\/original_end_tidal_co2_microstream_adult_sensor_m1920a_for_ph_ilips_patient_monitors.jpg","attrs":{"Price":"USD 16.1-50","Compliance":"FDA and CE certified","Model Number":"End-tidal CO\u2082 Microstream","Sterilization Method":"Ethylene oxide (EO) sterilized or gamma sterilized"}}
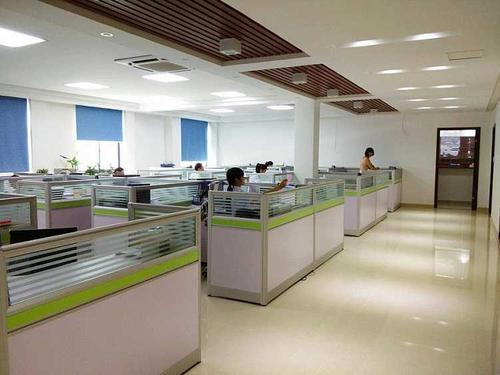
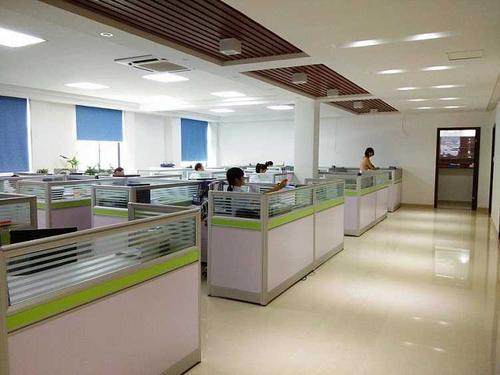
Shenzhen Better Love Medical Technology Co., Ltd. is a professional supplier specializing in original and compatible medical cable connectors, as well as medical electronic equipment accessories and consumables.
Our comprehensive product portfolio includes disposable and reusable pulse oximeter sensors, ECG monitoring leads, 12-lead EKG machine cables, SpO2 adapter cables, ECG electrode pads, NIBP cuffs, metal connectors, air hoses, medical-grade batteries, equipment modules, humidifier chambers, sampling tubes, ECG/monitor adapter cables, disposable temperature sensors, invasive blood pressure sensor cables, blood pressure cuff kits and various other connecting accessories.
Our products apply to a wide spectrum of medical instruments, including multi-parameter patient monitors, pulse oximeters, electrocardiograph (ECG) machines, ECG systems, electroencephalograph (EEG) devices, ultrasound systems, fetal monitors and defibrillators. With complete product specifications available, we ensure reliable compatibility with most imported and domestic device models.
Our products have been exported to more than 60 countries and regions across the globe, and are well recognized and trusted by customers worldwide.
Basic Information
Company Name:
Shenzhen Beijiaai Medical Technology Co., Ltd.
Business Type:
Manufacturer
Brands:
JHK
Employee Number:
50~150
Year Established:
2016
Total Sales Annual:
10000000-50000000
Company Location:
No. 101, Pai Fang Road, Xiang Fen Community, Xiu Xin Sub-district, Qian Zi Street, Ping An District, Shenzhen City, Guangdong Province
Factory Location:
No. 101, Pai Fang Road, Xiang Fen Community, Xiu Xin Sub-district, Qian Zi Street, Ping An District, Shenzhen City, Guangdong Province
Trade & Market
Company slogan:
Quality Consumables for Global Healthcare
OEM Overview:
With over 12 years of specialized experience and two self-operated production factories, we deliver full-cycle OEM/ODM solutions spanning consulting, design, R&D, prototyping and mass production for global medical brands and distributors.
Our customization covers 7 core product categories: vital signs monitoring modules & cables, vital signs detection equipment, disposable endoscope consumables, defibrillation products, operating room disposable consumables, rehabilitation & pelvic floor consumables, and bespoke medical device development. All customized orders are managed under strict ISO 13485 quality systems, with flexible MOQ and dedicated project tracking to ensure consistent quality and on-time delivery.
Production Line:
Shenzhen Better Love Medical Technology Co., Ltd. is a professional manufacturer specializing in the R&D, production and sales of patient monitoring medical consumables. Our core product range includes disposable and reusable SpO2 sensors, ECG/EKG cables, temperature probes, IBP cables, NIBP cuffs, defibrillation electrode pads, fetal probes and respiratory consumables, all widely compatible with mainstream medical device brands across the globe.
We operate under a strict ISO 13485 certified quality management system, and most of our products carry CE marking in full compliance with EU MDR regulations. Adopting a customer-first business philosophy, we serve hospitals, medical device distributors, brand owners and OEM partners in more than 50 countries and regions, delivering reliable, cost-effective medical supply solutions for global clinical applications.
Production Line
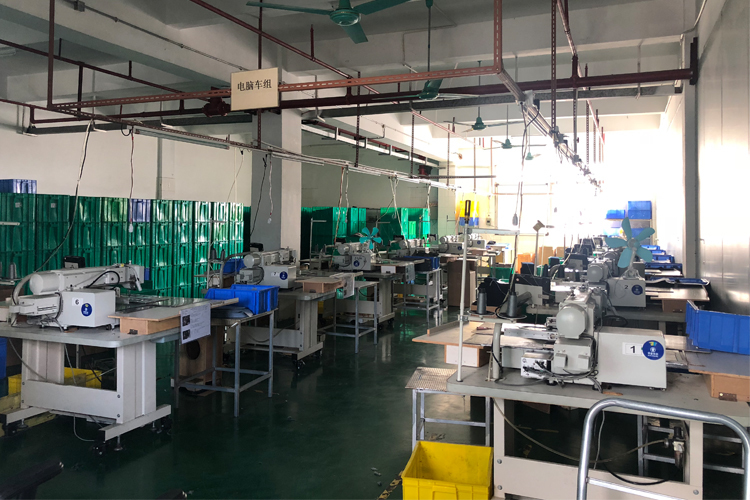
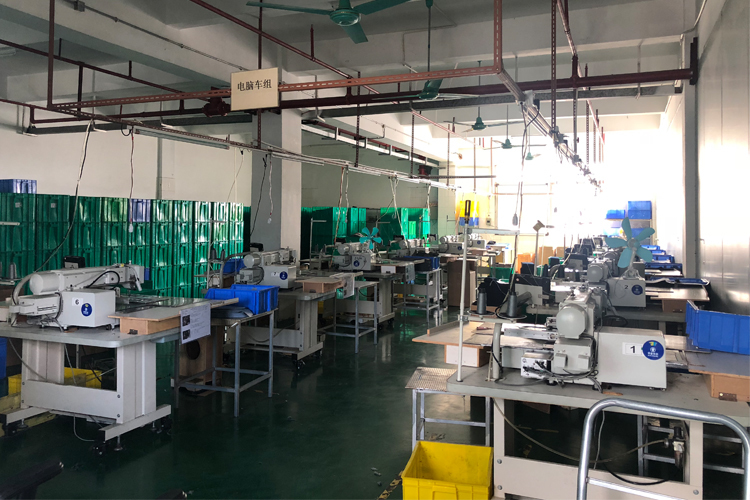
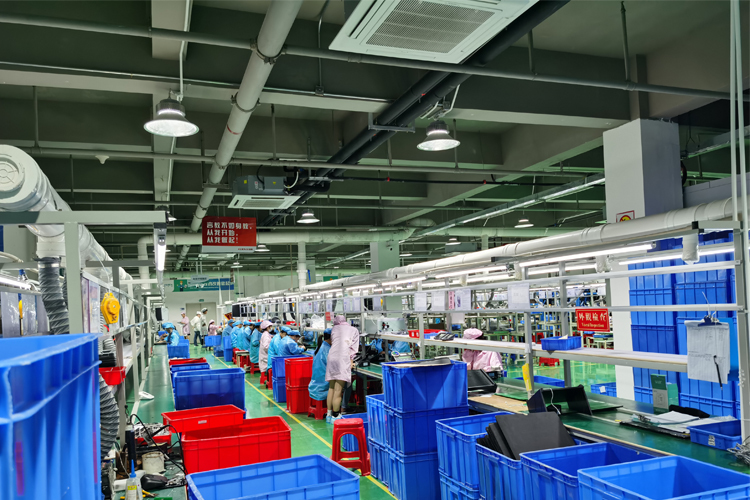
We run a modern production base equipped with standardized dust-free workshops and automated production lines, which enables stable mass output while guaranteeing consistent product quality across every batch.
Our full production workflow is fully traceable and managed under ISO 13485 standards:
Incoming Quality Control (IQC)
All raw materials — including medical-grade TPE and silicone, high-precision optical chips and medical connectors — go through strict inspection upon arrival. Unqualified materials are rejected directly to secure quality from the source.
Standardized Manufacturing
We deploy automatic soldering machines, cable forming equipment and laser marking systems to minimize manual deviation and improve production efficiency. Core assembly processes are completed in class 100,000 clean workshops to meet hygiene requirements for medical device production.
In-process Quality Control (IPQC)
Full-time quality inspectors conduct spot checks at each production stage to identify and resolve issues in real time, ensuring all semi-finished products meet specification requirements before proceeding to the next process.
100% Finished Product Inspection
Every finished unit undergoes full functional and appearance testing before packaging, including signal accuracy verification, tensile strength test, air tightness test (for pneumatic products) and biocompatibility spot check.
Sterilization & Traceable Packaging
Disposable products are sterilized by ethylene oxide (EO) with complete sterilization validation records, and individually packed in sterile blister packages marked with unique lot numbers, production dates and expiration dates for full traceability.
With a monthly production capacity of over 150,000 pieces of probes and cables, we are capable of fulfilling both small-batch trial orders and large-volume bulk contracts with stable and predictable lead times.
R&D:
Our in-house R&D team masters core technologies including high-precision optical sensing, bioelectric signal processing and biocompatible material application, ensuring our products reach original OEM-level measurement accuracy and anti-interference performance.
We adopt a compliance-driven R&D philosophy, closely tracking EU MDR, FDA and other global regulatory updates to reduce market access risks for partners. We launch 3–5 new or optimized products annually, and provide exclusive custom development services to help partners turn innovative product ideas into compliant, market-ready solutions efficiently.
Our Team:
Our core team has 12 years of hands-on experience in patient monitoring medical consumables, covering R&D, quality control, international sales and compliance support, to deliver full-range services for medical partners worldwide.
Our R&D team is familiar with compatibility tuning and custom development for all types of monitoring consumables, and can efficiently support OEM/ODM requirements. Our QC team follows ISO 13485 standards across the entire production process, with strict inspections from raw material arrival to finished product delivery, to ensure stable product quality and regulatory compliance.
Our international sales team knows well the rules of regional markets, and provides product selection advice, order follow-up and cross-border logistics support for customers in over 60 countries and regions with smooth, efficient communication. Our compliance staff keep up with regulatory updates such as EU MDR and US FDA, and can provide full certification documents to assist customers with customs clearance and local market access.
All core technical and service staff have received systematic professional training and hold relevant qualifications. We offer multilingual support with prompt response and smooth cooperation.
History:
Our Development Journey
Inheriting craftsmanship and advancing through innovation, we have built 12 years of professional expertise in the R&D and manufacturing of patient monitoring medical consumables, with a clear path of steady growth and global expansion.
2012: Foundation & European Market Entry
Founded in Shenzhen with a core focus on compatible SpO2 sensors and ECG cables, we rolled out our first generation of self-developed monitoring consumables. We obtained EU CE certification in the same year, officially entering the European market with products widely recognized for accurate measurement and stable quality.
2015: Global Expansion & FDA Clearance
We established a dedicated international business division to develop Southeast Asian, Middle Eastern and Latin American markets, and set up our first overseas technical support station. Our core product line obtained US FDA 510(k) clearance in the same year, successfully opening access to the North American market.
2018: Full Product Line Layout
We completed the strategic expansion of respiratory and anesthesia consumables, achieving full coverage of supporting consumables for patient monitoring scenarios. All products are manufactured under strict medical-grade quality standards to meet diversified clinical and commercial demands.
2021: Intelligent Manufacturing Upgrade
We deployed Industry 4.0 intelligent production lines to realize digital management across the entire production process, with annual output reaching tens of millions of units. We were also certified as a National High-Tech Enterprise in recognition of our independent R&D capabilities.
2024: MDR Regulatory Upgrade
Proactively adapting to evolving global medical device regulations, we completed full EU MDR certification for our core product range. This milestone confirms our quality management system meets the latest EU requirements for product safety, full traceability and risk management.
2025: New Self-Owned Production Base
Our brand-new self-owned production base was fully commissioned, tripling the workshop area and boosting annual production capacity by over 50%. The upgraded facility enables end-to-end quality control, intelligent manufacturing and more stable long-term supply for all global partners.
Guided by the philosophy of "quality first, innovation-driven", we have evolved from a single-product manufacturer to a comprehensive medical consumables solution provider. Today we serve clients in more than 60 countries and regions, and remain committed to delivering reliable, compliant products and professional, efficient services.
Service:
Shenzhen Beijiaai Medical provides comprehensive one-stop solutions for global medical distributors, hospitals and brand partners, focused on high-quality patient monitoring consumables and accessories.
Full-Range Product Supply
We offer a complete portfolio of disposable and reusable SpO2 sensors, ECG/EKG cables, temperature probes, IBP cables, NIBP cuffs, defibrillation electrodes, fetal probes and respiratory consumables, with reliable compatibility with mainstream brands including PH-ILIPS, Mindray, Nihon Kohden, Si-emens, Edan, Ma-siMo and Nell-cor.
OEM/ODM Customization
Backed by 12+ years of industry experience and two self-operated production facilities, we deliver end-to-end OEM/ODM services covering brand labeling, specification tuning and exclusive product development. All custom projects are governed by ISO 13485 quality systems with flexible MOQ terms.
Technical & After-Sales Support
Our professional engineering team provides accurate model matching, parameter consultation and full after-sales technical guidance, helping customers resolve compatibility issues and product application problems efficiently.
Global Delivery Service
We support both small-batch trial orders and large bulk purchases. With stable monthly production capacity and mature partnerships with top international logistics carriers, we ensure reliable on-time delivery to over 60 countries and regions worldwide.
Regulatory Compliance Support
Our core products are certified under ISO 13485, CE (MDR), FDA 510(k) and other global regulatory standards. We provide full certification dossiers and Certificates of Free Sale (CFS) to assist with customs clearance and local market access.
Factory Information
Market name:
North America,South America,Western Europe,Eastern Europe,Eastern Asia,Southeast Asia,Middle East,Africa,Oceania,Worldwide